Healthcare & Medical
https://www.taiwanunionplastic.com/healthcare-medical-injection-molding-machine/
#medical #injection #molding #machine
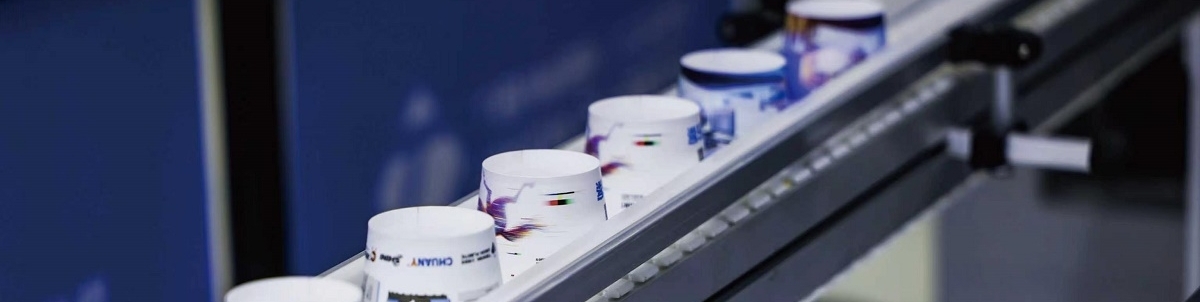
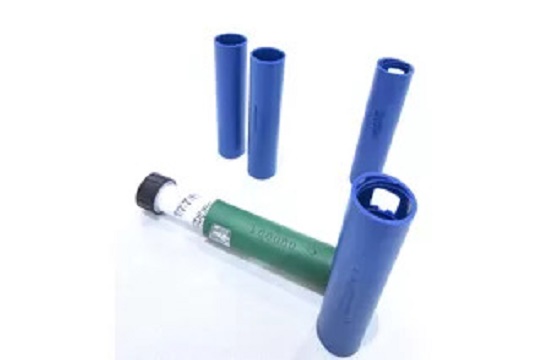
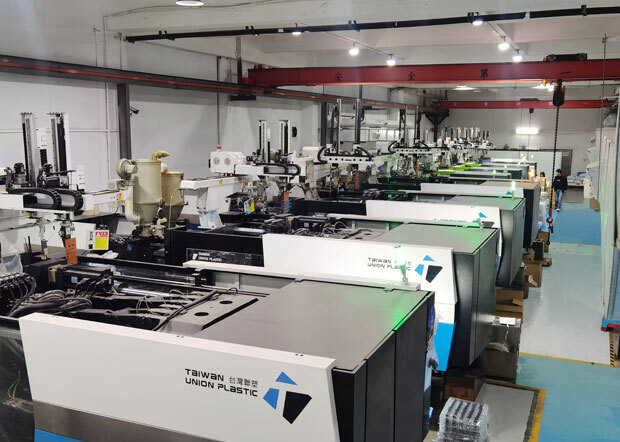
Cleanliness, High Precision, Traceability.Suitable For Medical Consumables And Aseptic Instrument Housings.Applicable To Syringe Barrels, Infusion Sets, Surgical Instrument Handles, As Well As Medical Housings And Accessories Respectively.
Healthcare & Medical
Our medical injection molding machine solutions are designed for medical-grade clean molding,... moreHealthcare & Medical
https://www.taiwanunionplastic.com/healthcare-medical-injection-molding-machine/
#medical #injection #molding #machine
Cleanliness, High Precision, Traceability.Suitable For Medical Consumables And Aseptic Instrument Housings.Applicable To Syringe Barrels, Infusion Sets, Surgical Instrument Handles, As Well As Medical Housings And Accessories Respectively.
Healthcare & Medical
Our medical injection molding machine solutions are designed for medical-grade clean molding, covering disposable precision medical consumables as well as large medical appearance and structural parts.
By adopting dedicated medical injection molding machine models and clean-production standards, manufacturers can achieve dimensional accuracy, stable performance, and controlled production that meets the medical industry's strict requirements for quality, compliance, and precision.
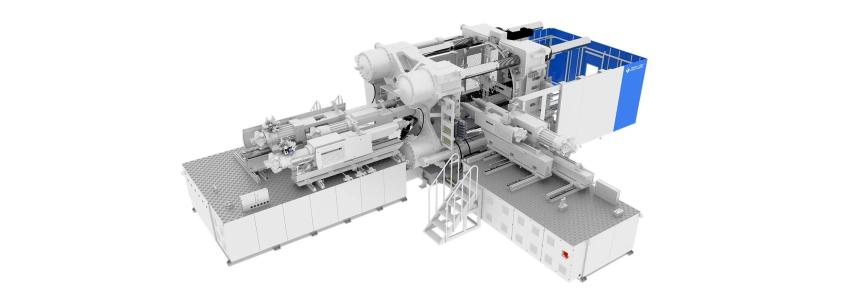
hs-d Two-Platen Multi-Component Injection Molding Machine
https://www.taiwanunionplastic.com/products/hs-d-two-platen-multi-component-injection-molding-machine/
#two #platen #injection #molding #machine
If you are seeking a stable, efficient and high-quality large-scale multi-color injection molding solution, then the HS-D two-part multi-color series with vertical turntable and two-part mold locking structure is the perfect choice for you.
Suitable for Large Molds
The larger ejection strok... morehs-d Two-Platen Multi-Component Injection Molding Machine
https://www.taiwanunionplastic.com/products/hs-d-two-platen-multi-component-injection-molding-machine/
#two #platen #injection #molding #machine
If you are seeking a stable, efficient and high-quality large-scale multi-color injection molding solution, then the HS-D two-part multi-color series with vertical turntable and two-part mold locking structure is the perfect choice for you.
Suitable for Large Molds
The larger ejection stroke and mold capacity make this two platen injection molding machine suitable for installing large molds and supporting a wider range of applications.
01
Vertical Turntable Structure
Diameter of the turntable is 3000mm, and it can bear a load of 38t.
02
More Comprehensive Processes
The flexible center-distance structure allows the two platen injection molding machine to be combined with multi-angle injection stations to meet diverse and customized production requirements.
Functional Advantages
Two-Platen Stucture
Highly rigid molds, with uniform force distribution; high-pressure mold-locking hydraulic cylinders, with locking position accuracy of ±0.2mm
Independent control of servo hydraulic system, energy-saving effect improved by 20%
High-torque material-mixing motors enable the two platen injection molding machine to support the production of large automotive parts, household appliance components, and other multi-color molded products
Multi-action synchronization, shortening the cycle time
European imported controllers and independently developed TUP software, fully optimizing machine operation, control and molding
Vertical Turntable Structure
The servo motor controls the 180° forward and reverse rotation of the turntable, and jointly positions the positioning cylinder to further control the accuracy of the turntable.
A pusher device is set on the back of the turntable to reduce the contact friction between the turntable rotation and the moving template.
The turntable gear is built-in, which increases the size of the mold installation surface and is suitable for a wider range of mold installations.
The TUP multiple turntable patent devices are configured to prevent common problems such as the turntable tilting under heavy load.
Multi-Angle Injection Station
The injection and plasticizing system adopts linear guide rails with low friction coefficient.
The high rigidity single-cylinder injection structure and low inertia actuator design ensure fast response and high precision.
The flexible center distance structure can be combined with multi-angle injection stations to meet diverse and personalized requirements.
Two-Color and Multi-Component Injection Molding: Process, Machine Types, Material Decisions, and ROI
https://www.taiwanunionplastic.com/blog/two-color-and-multi-component-injection-molding-process-machine-types-material-decisions-and-roi.html
#Multi-component #machine
Table of Content [Hide]
1. What Is Two-Color Injection Molding?
2. What Is Multi-Component Injection Molding?
3. Two-Shot, Overmolding, Insert Molding, and Co-Injection: What Is the Difference?
4. How the Two-Color Injecti... moreTwo-Color and Multi-Component Injection Molding: Process, Machine Types, Material Decisions, and ROI
https://www.taiwanunionplastic.com/blog/two-color-and-multi-component-injection-molding-process-machine-types-material-decisions-and-roi.html
#Multi-component #machine
Table of Content [Hide]
1. What Is Two-Color Injection Molding?
2. What Is Multi-Component Injection Molding?
3. Two-Shot, Overmolding, Insert Molding, and Co-Injection: What Is the Difference?
4. How the Two-Color Injection Molding Process Works
5. Rotary Platen Multi-Component Injection Molding Machine
6. Core-Back and Core-Rotation Systems
7. Opposite-Injection and Multi-Angle Injection Structures
8. Two-Platen Multi-Component Injection Molding Machine for Large Parts
9. How to Choose Materials for Two-Shot and Multi-Component Molding
10. Mold Design Requirements for Two-Color Injection Molding
11. Injection Unit Sizing for Multiple Materials
12. Process Control and Quality Metrics
13. Automation and Safety in Multi-Component Production
14. How to Calculate ROI for a Two-Color Injection Molding Project
15. Two-Color Injection Molding vs Separate Molding and Assembly
16. Application Examples by Industry
17. Supplier and Machine Selection Checklist
18. Common Failure Modes and How to Prevent Them
19. How Taiwan Union Plastic Configures Multi-Component Machines
20. Frequently Asked Questions
21. Conclusion
22. External References
Two-color and multi-component injection molding allow manufacturers to integrate colors, materials, textures, sealing functions, soft-touch areas, transparent windows, decorative surfaces, or structural zones into one molded component. The process can remove assembly, improve alignment, reduce handling, and create features that are difficult to achieve with one material. It can also create expensive problems when material compatibility, mold transfer, injection-unit sizing, cooling balance, and process sequencing are treated as afterthoughts.
This guide helps engineers, mold makers, managers, and buyers decide whether the process is justified and which machine architecture fits. It distinguishes two-color, two-shot, multi-material, overmolding, insert molding, co-injection, and multi-component machine concepts; explains the main mechanical structures; provides a practical material and tooling checklist; and shows how to estimate the business value of integrating operations.
Taiwan Union Plastic (TUP) has developed hydraulic, hybrid, two-platen, opposite-injection, and multi-component machine configurations for products ranging from small two-color components to large automotive and appliance parts. The correct configuration begins with the final part and transfer sequence, not with a machine series name.
What Is Two-Color Injection Molding?
Two-color injection molding is a process in which two colored polymer shots are molded in a controlled sequence to form one finished part, usually within one automated molding cycle. The two shots may use the same resin family in different colors or different compatible materials when both appearance and function are required.
A common example is a rigid plastic product with two visible colors. The first cavity forms the base geometry. The mold or molded preform then moves to a second position, where another injection unit adds the second color. The transfer may be achieved by a rotating platen, rotating mold core, indexing plate, core-back movement, robot transfer, or another mechanism. The interface between shots must be located precisely so that the finished boundary is clean and repeatable.
The phrase “two-color” mainly describes appearance, but the engineering challenge is broader. The process must control first-shot shrinkage, surface temperature at the second shot, venting, injection balance, material bonding, flash, and the mechanical load created during rotation or transfer. A visually simple color boundary can therefore require a sophisticated mold and machine.
What Is Multi-Component Injection Molding?
Multi-component injection molding is a manufacturing process in which two or more polymer components are injected sequentially or in coordinated stages to create a single integrated molded part. The components may differ in color, hardness, transparency, chemical resistance, friction, conductivity, barrier performance, or other functional properties.
Multi-component molding includes more than two-color products. It can combine a rigid substrate with a soft thermoplastic elastomer grip, create a clear window in an opaque housing, integrate a seal into a connector, mold several colors into an automotive light component, or produce layered structures with different performance zones. Depending on the part and mold, the machine may require two, three, four, or more injection units.
For procurement teams, the key distinction is that a two color injection molding machine is not defined only by the number of barrels. The clamping unit, rotary or transfer system, mold-interface accuracy, injection-unit positions, simultaneous movement capability, controller sequencing, and safety logic determine whether the production cell can execute the intended process reliably.
Two-Shot, Overmolding, Insert Molding, and Co-Injection: What Is the Difference?
Two-shot, overmolding, insert molding, and co-injection are related processes that combine materials, but they differ in how the first component is created, transferred, and enclosed by the next material. Clear terminology prevents buyers and suppliers from specifying the wrong mold or machine.
Process How It Works Typical Equipment Best Fit Main Risk
Two-shot molding Two materials or colors are injected in sequence in one integrated cycle Two injection units with rotary, indexing, or core-back system High-volume integrated parts Material bonding and transfer alignment
Overmolding A second material is molded over a previously molded substrate Two-shot cell or separate machines with manual/robot transfer Soft grips, seals, insulation, protection Substrate temperature, contamination, weak adhesion
Insert molding Metal, electronic, textile, or preformed inserts are placed in the mold and surrounded by resin Horizontal or vertical machine with manual/robot loading Threaded inserts, terminals, reinforced parts Insert movement, damage, incomplete encapsulation
Co-injection or sandwich molding Materials create a skin-core or layered structure through controlled flow paths Special multi-component injection system Barrier, recycled core, structural layering Unstable layer distribution and breakthrough
Multi-color molding Two or more colored shots create visual zones Multi-component machine and precision transfer mold Consumer, automotive, appliance and decorative parts Color contamination and boundary mismatch
A part can use more than one concept. In two color molding, the two shots typically create separate visual zones, while a three-component product may include a rigid first shot, a clear second shot, and a soft third-shot seal. A metal insert may be loaded before a two-color sequence begins. The user requirement specification should describe the complete cycle in numbered steps so that the machine builder, mold maker, material supplier, robot integrator, and buyer share the same process definition.
How the Two-Color Injection Molding Process Works
The two color injection molding process is a sequenced production cycle in which the first shot creates a substrate, the mold or part changes position, and the second shot forms the final color or material zone. A stable process depends on both shots remaining within a common thermal, mechanical, and timing window.
Mold closing and protection:
The machine closes the mold while monitoring position, force, and obstruction conditions.
First-shot injection:
The first injection unit fills and packs the substrate cavity.
Partial cooling:
The first shot cools enough to retain shape during transfer but may need sufficient surface heat for bonding.
Transfer or rotation:
The platen, core, indexing plate, or robot moves the first shot into the second-shot cavity.
Second mold closing:
The mold closes around the transferred substrate with controlled alignment.
Second-shot injection:
The second material or color fills the remaining cavity and bonds or mechanically locks to the first shot.
Final cooling:
Both materials cool while differential shrinkage and interface stress develop.
Ejection and handling:
The completed part is ejected, inspected, and transferred to downstream operations.
The correct timing between shots is critical. If the first shot is too hot, it may deform under the second-shot pressure. If it is too cold, chemical bonding may weaken. If transfer takes too long, the surface can cool or become contaminated. If the first shot shrinks away from the second cavity, flash, mismatch, or poor support may occur.
Successful process development therefore requires a documented window for first-shot melt temperature, mold temperature, cooling time, transfer time, second-shot melt temperature, injection speed, transfer position, holding pressure, and final cooling. The machine controller should store the sequence, monitor deviations, and provide enough data for troubleshooting.
Rotary Platen Multi-Component Injection Molding Machine
A rotary platen multi-component injection molding machine uses a rotating section of the clamping system to move the first-shot molded substrate from one cavity position to another. It is one of the most common structures for high-volume two-color and two-material parts because transfer is integrated into the machine cycle.
After the first shot, the mold opens to the required distance, the rotary platen turns by a defined angle, and the first-shot core aligns with the second-shot cavity. The system must control rotation speed, stopping accuracy, locking, mold cable and hose routing, mold weight, inertia, and safety. Larger molds create higher rotational loads and require stronger bearings, supports, and drive systems.
TUP states that the turntable on its HD multi-component series is servo driven, with rotation speed increased by 50% and action accuracy improved by 60% compared with the company’s stated reference configuration. These figures indicate the importance of transfer performance, but buyers should ask which model, load, diameter, rotation angle, and test method apply to the quoted machine.
Rotary platen systems are suitable for toothbrush handles, tool grips, appliance controls, lids, consumer products, automotive trim, lighting components, seals, and other parts in which the first shot can remain on the rotating core. The mold design must account for balanced first- and second-shot operations because the two sides often run simultaneously after the start-up cycle.
Core-Back and Core-Rotation Systems
Core-back and core-rotation systems create the second-shot cavity by moving or rotating a mold component rather than rotating the complete platen. These methods can reduce the mass being moved and are useful when the product geometry supports an internal change in cavity volume or position.
In a core-back process, a movable core initially occupies the space intended for the second material. After the first shot forms, the core retracts to create a new cavity, and the second material fills the released volume. This can be efficient for seals, layered regions, handles, and products where the second shot surrounds or follows the first geometry.
Core rotation uses a rotating mold core to reposition the first shot. It may be appropriate for smaller parts or specialized geometries. The machine must provide hydraulic, pneumatic, electric, or mechanical interfaces to control the mold action, and the controller must confirm each position before injection.
The advantage of these systems is compact transfer. The disadvantage is that the mold becomes more complex, and maintenance access, cooling, sensing, sealing, and mechanical wear require careful design. The machine supplier and mold maker should jointly review the required interfaces before the mold is released for manufacturing.
Opposite-Injection and Multi-Angle Injection Structures
Opposite-injection and multi-angle injection structures position additional injection units at different sides or angles around the mold so that materials can enter from directions suited to the product geometry. These configurations are useful when conventional parallel injection units cannot reach the required gate locations or when a large complex part requires several material zones.
An opposite-injection machine can place injection units on opposing sides of the clamping area. This arrangement can support large multi-color products, thick sections, automotive lighting, appliance panels, and other parts where balanced or separate directional filling is required. Machine design must consider injection-unit support, nozzle alignment, mold access, purging, maintenance space, and interaction with robots or mold-changing equipment.
Multi-angle systems may place an auxiliary injection unit vertically, horizontally, or diagonally. The position can be fixed or adjustable depending on the design. Buyers should verify injection-unit weight support, center-distance range, nozzle force, screw size, pressure capability, material feed access, and whether the unit can be removed or repositioned for other molds.
The process specification must show every gate and material flow path. A statement such as “three colors” is not enough to select the machine. The supplier needs a mold concept, part orientation, shot weights, resin data, injection sequence, and required unit positions.
Two-Platen Multi-Component Injection Molding Machine for Large Parts
A two-platen multi-component injection molding machine combines a compact large-mold clamping architecture with multiple injection units and a transfer system for producing large two-color or multi-material components. It is particularly relevant when mold dimensions, opening stroke, platen space, and rotary load exceed the practical range of a smaller conventional machine.
Large automotive, appliance, logistics, and decorative components can require both high clamping force and complex material integration. A two-platen structure can provide generous mold capacity and opening space while keeping the machine length manageable. The challenge is maintaining platen parallelism, mold support, transfer accuracy, and stable injection sequencing under heavy loads.
TUP’s HS-D series uses a two-platen clamping structure with a vertical turntable. The company describes a turntable diameter of 3,000 millimeters and a load capacity of 38 tons for the stated configuration. These values demonstrate the scale of molds that may be handled, but they must be matched to the quoted model, mold center of gravity, rotation speed, opening stroke, and foundation requirements.
For buyers considering a two platen injection molding machine, provide the complete mold assembly weight, rotating mass, diameter, thickness, utility connections, moving-core system, and intended installation method. A machine can have sufficient nominal clamping force but still be unsuitable if the mold envelope, rotary inertia, or support conditions are not compatible.
How to Choose Materials for Two-Shot and Multi-Component Molding
Material selection for two-shot and multi-component molding is the process of verifying that each resin meets its own performance requirements and can also survive the thermal, chemical, mechanical, and dimensional interaction with the other component. A material pair that looks compatible in a general chart may still fail in a specific geometry or operating environment.
Evaluate at least the following factors:
Chemical adhesion:
Determine whether the materials can form a reliable bond under the selected melt and mold temperatures.
Mechanical interlocking:
Add holes, ribs, undercuts, grooves, or wraparound features when chemical adhesion is uncertain or insufficient.
Melt-temperature compatibility:
The second-shot temperature must not excessively soften, degrade, or distort the first shot.
Mold-temperature compatibility:
Both materials must process within a mold-temperature range that supports filling, surface quality, bonding, and release.
Shrinkage and thermal expansion:
Different shrinkage rates can cause warpage, peeling, residual stress, or dimensional change.
Moisture and contamination:
Hygroscopic materials require correct drying, and mold-release agents or surface contamination can weaken bonding.
Service environment:
Test temperature cycling, chemicals, UV, humidity, sterilization, fatigue, oils, cleaners, and mechanical loads as relevant.
Color and migration:
Pigments and additives can influence bonding, staining, bleeding, surface appearance, and regulatory status.
Do not approve a material pair based only on generic polymer families. Commercial grades contain fillers, lubricants, flame retardants, impact modifiers, stabilizers, and color packages that can change adhesion and shrinkage. Use the exact production grades during validation.
Prototype plaques can screen adhesion, but the final part geometry matters. A peel test on a flat plaque may not represent stress at a sharp corner or thin seal. Define test methods that reflect product use: peel, pull, torque, pressure, leak, thermal cycling, drop, flex, chemical exposure, sterilization, or accelerated aging.
Mold Design Requirements for Two-Color Injection Molding
Two-color mold design is the coordinated design of cavities, cores, transfer mechanisms, gates, vents, cooling circuits, shutoffs, and interfaces that allow multiple materials to form one part without flash, mismatch, damage, or unstable bonding. The mold is often the most technically demanding element of the project.
In two color molding, the first-shot part must remain on the intended core during mold opening and transfer. Retention features, shrinkage direction, draft, surface finish, ejector placement, and cavity pressure all influence where the substrate stays. If it remains on the wrong side, the process cannot continue automatically.
The second-shot cavity must support the first shot against injection pressure. Unsupported thin areas can deform. Shutoff surfaces need sufficient strength and precision to prevent material from leaking across the color boundary. Venting is critical because the first shot can block normal air escape paths. The mold should also prevent the second material from entering areas where it could create flash or interfere with assembly.
Cooling balance is more complex than in a single-shot mold. The first and second shots may have different wall thicknesses and resins. If one side cools much faster, simultaneous production can become unbalanced. The mold designer may need separate temperature circuits, inserts, conformal cooling, or controlled delays.
Rotary molds require reliable connection management for water, hydraulics, pneumatics, hot runners, sensors, and electrical circuits. Rotary unions, protected hose paths, quick connections, and position sensing should be planned early. Service access must be possible without disassembling unrelated systems.
Injection Unit Sizing for Multiple Materials
Injection-unit sizing is the process of matching each material shot to an appropriate screw diameter, shot capacity, injection pressure, injection rate, plasticizing rate, and residence-time range. In a multi-component machine, every injection unit must be sized independently because the shots can differ greatly.
A common mistake is to size the machine around total part weight while ignoring that one component may represent only a small fraction of the shot. If a 120-gram part contains a 6-gram soft seal, placing the seal material in a very large barrel can create excessive residence time and unstable metering. The auxiliary unit may need a much smaller screw even though the main machine is large.
At the other extreme, a small screw may lack the injection rate or pressure required to fill a long, thin second-shot feature. Screw size affects both shot capacity and flow capability. The resin’s viscosity, gate size, flow length, wall thickness, mold temperature, and allowable shear must be considered.
Plasticizing time must fit the cycle. If the second material recovers too slowly, it becomes the cycle limiter. If it recovers too quickly at excessive screw speed, the material may overheat or degrade. Each unit needs an appropriate screw design for the resin, filler, shear sensitivity, and color-change requirement.
Process Control and Quality Metrics
Process control in the two color injection molding process requires coordinated monitoring of both material shots, transfer movements, mold positions, temperatures, pressures, and timing so that the interface and final part remain consistent. A part can pass overall weight inspection while still having a weak bond or incorrect material distribution.
Track separate process variables for every injection unit. These may include fill time, transfer position, peak pressure, pressure at transfer, cushion, holding profile, screw recovery time, back pressure, melt temperature, and material lot. Track the rotary or core-back sequence with position, time, torque, alarms, and lock confirmation.
Quality inspection should include more than visual color separation. Depending on the product, measure:
First-shot and final part weight.
Color boundary position and flash width.
Bond strength or peel force.
Seal compression, leak rate, or pressure retention.
Warpage and dimensional change after conditioning.
Surface defects, flow marks, weld lines, burn marks, and contamination.
Functional torque, pull force, impact, or flex life.
Material presence using vision, sensors, X-ray, CT, or sectioning where appropriate.
A scientific process-development approach should establish a stable window rather than one optimized setpoint. The team should understand how far injection speed, melt temperature, mold temperature, holding pressure, and transfer time can vary before the part fails. This information supports faster recovery after maintenance, material-lot changes, or mold transfer.
Automation and Safety in Multi-Component Production
Automation in multi-component production coordinates inserts, material handling, mold transfer, robots, inspection, degating, assembly, and packing around a more complex molding sequence. The automation plan must be designed with machine guarding and process recovery in mind.
Robots may load inserts, remove first-shot preforms for transfer between machines, place labels, inspect color boundaries, separate rejects, or pack finished parts. When the machine itself rotates a platen or mold, the robot path must avoid the rotary envelope, hoses, auxiliary injection units, and mold-protection zones.
Safety interlocks should confirm guards, operator gates, transfer positions, rotary locks, core positions, robot home positions, and injection-unit status before hazardous movement begins. ISO 20430 addresses significant hazards for hydraulic and electrical injection molding machines, while OSHA guidance illustrates guarding, operator gates, purge guards, emergency stops, and robot hazards on horizontal molding machines.
Recovery after an interrupted cycle deserves special attention. If the process stops after the first shot but before the second, the machine needs a controlled method to remove or classify the incomplete part. Restarting with an old first shot can create a bond failure. The controller should identify cycle stage, and work instructions should define how the operator clears the mold safely.
How to Calculate ROI for a Two-Color Injection Molding Project
Return on investment for the two color injection molding process is the financial benefit created by integrating materials or colors into the molding cycle compared with the total additional cost of the machine, mold, development, maintenance, and process complexity. The strongest projects remove recurring labor, fixtures, adhesives, inventory, and quality risk at sufficiently high production volumes.
Start with the current process. Assume a product is molded as two separate parts and then assembled. The annual volume is 2,000,000 units. Assembly labor and equipment cost $0.055 per unit, adhesive and consumables cost $0.018, and assembly-related scrap or rework costs $0.012. The total avoidable recurring cost is $0.085 per unit, or $170,000 per year.
The multi-component project requires an additional $260,000 for machine capability, mold complexity, robot integration, testing, and training. It also adds $25,000 per year in maintenance, validation, and more complex changeovers. Net annual benefit is $170,000 − $25,000 = $145,000. The simple payback is $260,000 ÷ $145,000 = 1.79 years.
This model is incomplete until cycle and capacity are included. If the integrated cycle is 18 seconds and the current molding plus assembly system effectively produces a finished part every 14 seconds, the new cell may require more cavities or another machine. Conversely, if assembly is the bottleneck and the integrated process increases accepted output, capacity value may exceed direct labor savings.
Also calculate avoided inventory and quality cost. Separate components require work-in-process storage, matching, transportation, and traceability. Adhesive curing can require floor space and waiting time. Manual assembly can introduce orientation errors or incomplete seating. A multi-component part can eliminate these risks, but it may also concentrate failure: a defect in either shot rejects the entire part.
Two-Color Injection Molding vs Separate Molding and Assembly
Two-color injection molding and separate molding plus assembly are alternative production routes that should be compared by annual volume, design stability, process flexibility, capital, quality risk, and lifecycle cost. Integrated molding is not automatically the better choice for low-volume or frequently changing products.
Factor Two-Color / Multi-Component Molding Separate Molding and Assembly
Capital investment Higher machine and mold complexity Lower initial tooling may be possible
Unit labor Can eliminate assembly and adhesive operations Ongoing assembly labor and equipment
Alignment Controlled by mold and transfer system Controlled by fixtures, operators, or assembly machines
Material bond Chemical and/or mechanical bond created during molding Fasteners, welding, adhesive, or mechanical fit
Design changes Changes may affect complex integrated tooling Individual components can sometimes be changed independently
Scrap impact Failure in either shot can reject the full part Defective components may be separated before assembly
Best volume Medium to high stable volume Prototype, low volume, variable mix, or uncertain design
For a new product with uncertain demand, a staged approach may be safer. Begin with separate molding and assembly to validate the market, then convert to multi-component tooling after the design and volume stabilize. For an established high-volume product with significant assembly cost, integrated molding may justify the investment immediately.
Application Examples by Industry
Multi-component injection molding applications are products that gain measurable value from combining colors, materials, surfaces, seals, or functions in one controlled molding process. Two color molding is especially suitable when manufacturers need repeatable color separation while reducing secondary painting, assembly, or decoration operations. The best applications use integration to solve a product or production problem, not merely to add complexity.
Automotive:
Light lenses and housings, interior controls, decorative trim, seals, soft-touch surfaces, air vents, and multi-color exterior components.
Medical:
Syringe closures, seals, grips, device housings, fluid-path components, and parts requiring hard-soft integration.
Consumer products:
Toothbrushes, razors, tool handles, kitchenware, buttons, lids, toys, and sports products.
Electronics:
Connector seals, cable interfaces, keypads, protective corners, display windows, and insulating zones.
Home appliances:
Control panels, windows, knobs, handles, decorative components, and vibration-damping elements.
Packaging:
Two-color closures, integrated seals, decorated lids, and functional barrier or grip features.
Industrial products:
Gaskets, wheels, rollers, dampers, anti-slip surfaces, protective housings, and components with localized performance requirements.
Supplier and Machine Selection Checklist
A multi-component machine selection checklist is a structured set of technical and commercial questions used to verify that the supplier can support the complete molding sequence, not just provide multiple injection units. The machine, mold, automation, materials, and process must be engineered as one system.
How many components, colors, and injection units are required?
What are the exact shot weights, materials, melt temperatures, pressures, and injection-rate targets for each unit?
Which transfer method is used: platen rotation, core rotation, indexing plate, core-back, robot transfer, or opposite injection?
What is the rotating mold weight, diameter, center of gravity, inertia, and required positioning accuracy?
Can the mold and injection units fit within the platen, tie-bar, nozzle, and service-space limits?
Can both shots plasticize within the target cycle?
Which movements can occur simultaneously, and under what safety conditions?
How are water, hydraulics, pneumatics, hot runners, sensors, and electrical circuits managed during rotation?
What process data can be stored, exported, alarmed, and connected to MES?
How will incomplete first-shot parts be detected and removed?
What FAT will prove cycle time, transfer accuracy, part quality, bond strength, and energy use?
Who coordinates the machine, mold, robot, material, and process-development responsibilities?
TUP’s injection molding solutions cover equipment, molding processes, industry applications, and turnkey planning. For a multi-component project, the most valuable early step is a joint technical review using the part drawing, mold concept, material data, cycle sequence, and output target. This reduces the risk of discovering an interface conflict after the machine or mold has already been manufactured.
Common Failure Modes and How to Prevent Them
Common multi-component molding failures are defects caused by unstable transfer, incompatible materials, incorrect thermal conditions, poor mold support, imbalanced cooling, or uncontrolled sequencing. Because several operations are integrated, troubleshooting must separate first-shot, transfer, and second-shot effects.
Weak bonding:
Verify exact resin grades, surface contamination, first-shot temperature, second-shot melt temperature, pressure, contact area, and mechanical interlocks.
First-shot deformation:
Increase support, adjust cooling, reduce second-shot pressure peak, or change the sequence and gate design.
Flash at the interface:
Improve shutoff design, mold alignment, first-shot dimensions, clamp conditions, and transfer accuracy.
Color boundary mismatch:
Inspect rotary stop position, mold wear, first-shot shrinkage, cavity pressure, and core locking.
Part remains on the wrong mold half:
Adjust draft, texture, retention, cooling, ejection, and shrinkage direction.
Warpage:
Balance shrinkage, wall thickness, cooling, packing, material orientation, and post-mold conditioning.
Cycle imbalance:
Resize injection units, improve cooling, adjust simultaneous movements, or change cavity allocation.
Material contamination:
Improve drying, purge procedures, hopper separation, color-change control, and housekeeping.
Use short-shot studies and separate first-shot inspection during development. A final defect may originate in the first shot even when it becomes visible only after the second material is added. Save process data for both units and correlate it with quality measurements.
How Taiwan Union Plastic Configures Multi-Component Machines
Taiwan Union Plastic configures multi-component injection molding machines by combining clamping architecture, injection-unit layout, transfer structure, control sequence, and industry-specific process requirements. The company’s range includes conventional multi-component hydraulic platforms, opposite-injection machines, two-platen multi-component systems, and hybrid multi-component options.
The HD series supports flexible injection-unit positioning for different multi-color applications. The HS-D series extends multi-component capability to large molds through a two-platen structure and vertical turntable. Opposite-injection and multi-angle arrangements can address large products or gate locations that cannot be served by standard parallel units. A hybrid injection moulding machine can add electric injection control where higher precision, faster response, and multi-component process flexibility are required.
A responsible proposal should state which machine functions are standard, which are customized, and which depend on the mold or automation supplier. It should also define the accepted rotating load, injection-unit specifications, mold interfaces, safety sequence, communication standard, testing plan, training, spare parts, and service scope. These details are more important than a general claim that the machine can produce multiple colors.
Frequently Asked Questions
This FAQ section answers common buyer and engineering questions.
What is the difference between two-color and two-shot injection molding?
Two-color molding emphasizes two visible colors, while two-shot molding emphasizes two sequential injection stages. Many projects are both two-color and two-shot. A two-shot part can also use different materials with the same color, such as a rigid substrate and a soft seal, so the terms are related but not identical.
Can any two plastics be used in multi-component injection molding?
No. The exact commercial grades must be tested for chemical adhesion, processing-temperature compatibility, shrinkage, thermal expansion, moisture sensitivity, additives, and service conditions. Mechanical interlocks can improve retention when chemical bonding is weak, but they must be designed for the actual loads and geometry.
Does a two-shot machine always reduce cycle time?
Not always. It can eliminate separate molding, handling, adhesive curing, and assembly, but the integrated molding cycle may be longer than either single-shot cycle. Evaluate finished-part output, cavity count, cooling, transfer time, automation, scrap, and total process capacity rather than comparing only machine cycle seconds.
When should a two-platen multi-component machine be used?
Use a two-platen multi-component platform when the project requires large molds, high clamping force, long opening stroke, generous mold space, and integrated multi-color or multi-material transfer. Automotive, appliance, logistics, and large decorative parts are common candidates, subject to mold weight and rotary-load verification.
What data is required for a multi-component machine quotation?
Provide the part drawing, material grades, shot weights, cavity count, mold concept, mold dimensions and weight, transfer method, injection-unit positions, cycle sequence, output target, automation scope, utilities, quality tests, and FAT requirements. A simple statement such as “two colors, 1,000 tons” is not sufficient for accurate selection.
How is bond strength tested in two-shot molded parts?
The test should reflect product use. Methods may include peel force, tensile pull, torque, pressure, leak, flex, impact, thermal cycling, chemical exposure, sterilization, or accelerated aging. Define the specimen location, conditioning, test speed, temperature, failure mode, and minimum acceptance value before production approval.
Conclusion
This conclusion summarizes the recommended decision and implementation approach.
Two-color and multi-component injection molding create value when they integrate functions that would otherwise require separate parts, assembly, adhesives, fixtures, inventory, or quality checks. The technology is most successful when the product design, exact material grades, mold transfer, injection-unit sizing, cooling balance, automation, quality tests, and machine sequence are developed together.
Rotary platen machines are efficient for many high-volume two-shot parts. Core-back and core-rotation systems can simplify transfer for suitable geometries. Opposite-injection and multi-angle layouts solve complex gate and large-part requirements. Two-platen multi-component machines extend the process to very large molds and high clamping forces. None of these structures is universally best; the part and mold determine the architecture.
Taiwan Union Plastic can evaluate multi-component projects across hydraulic, hybrid, opposite-injection, rotary, and two-platen platforms. Buyers who provide complete part, mold, material, cycle, and acceptance data will receive a more defensible machine selection and reduce the risk of costly changes late in the project.